Pick the wrong process, and the same part can cost far more, take weeks longer, or lock you into a design you can’t change.
Extrusion and CNC machining pull cost, lead time, and design freedom in completely different directions. That makes the choice trickier than it looks.
Here is the core tension. A constant cross-section made in high volume points to extrusion. Complex geometry, tight tolerances, and design flexibility point to CNC.
I have helped many clients find the right process for their parts. Here is how I think about it.
This guide gives you a clear decision framework, the real cost logic behind each option, and something most teams overlook: the hybrid route that blends both. By the end, you’ll know exactly which path fits your part.
Why This Decision Matters More Than It Looks
The process you pick doesn’t just shape the part. It shapes your whole budget, timeline, and how much room you have to change things later.
Here’s what I see go wrong.
A team opens an extrusion die for a part that keeps changing. The design shifts, the die no longer fits, and that tooling money is gone. You can’t unspend it.
Or a team picks CNC for a simple, constant-profile part made in large volumes. The unit price sits high and never drops. Machining charges by time, so every part costs about the same. Volume doesn’t rescue you.
Then come the surprises nobody quoted.
An extruded profile looks cheap on paper. But it still needs holes drilled, faces flattened, or threads cut. That secondary machining shows up as a fresh invoice weeks later.
Tolerance troubles pile on too. Push extrusion for tight features across a long length, and parts drift out of spec. Scrap climbs. Yield drops. Suddenly the “cheaper” route costs more than machining would have.
This is the point I want you to sit with.
Extrusion and CNC aren’t just two ways to make metal. They’re two different bets on cost, risk, and flexibility. The choice gets bigger the further you go, not smaller.
Treat it as a real engineering decision, made early, with the numbers in front of you. Get it right at the start, and the savings compound. Get it wrong, and you pay for that mistake in every unit you ship.
What Each Process Really Delivers
Both processes make solid parts. But they get there in opposite ways, and that difference decides everything downstream.
What hard alloy extrusion gives you
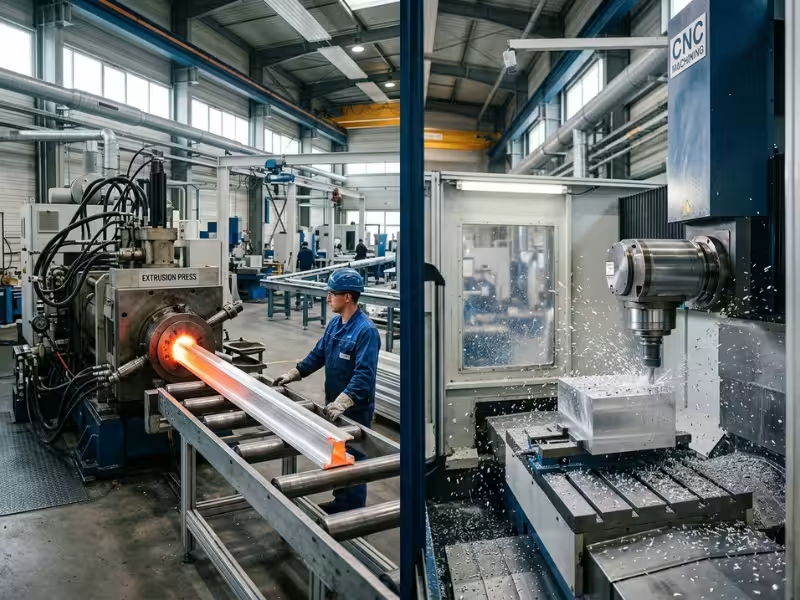
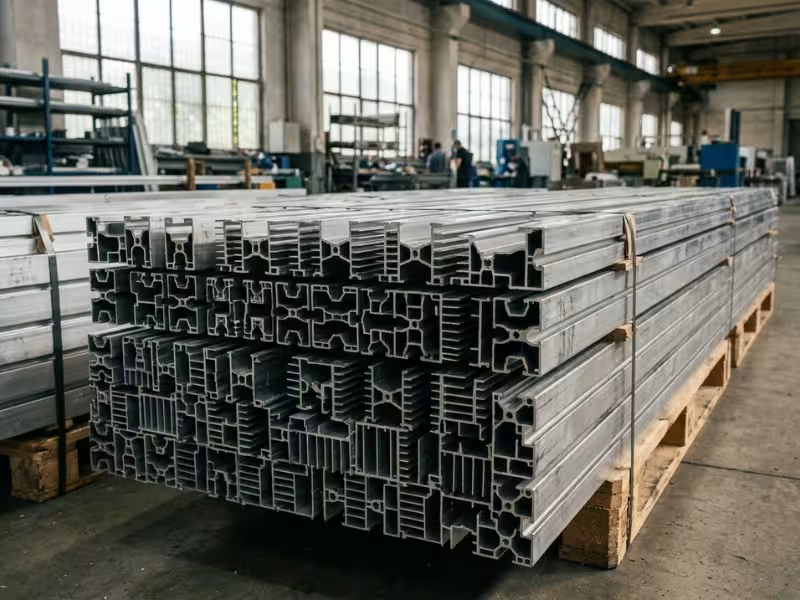
Extrusion pushes hot metal through a shaped die. The die defines the profile, and every part that follows carries that same cross-section down its length. Think rails, heat sinks, frames, or structural bars. Once the die exists, you can run thousands of parts fast and cheap. The per-part cost keeps dropping as volume climbs.
The catch is simple. Your geometry lives and dies by the die. You get a continuous profile and a near-net shape, but not much freedom beyond that. Holes, pockets, and features that break the cross-section are not part of the deal. Extrusion gives you an efficient blank, not a finished detail.
What CNC machining gives you
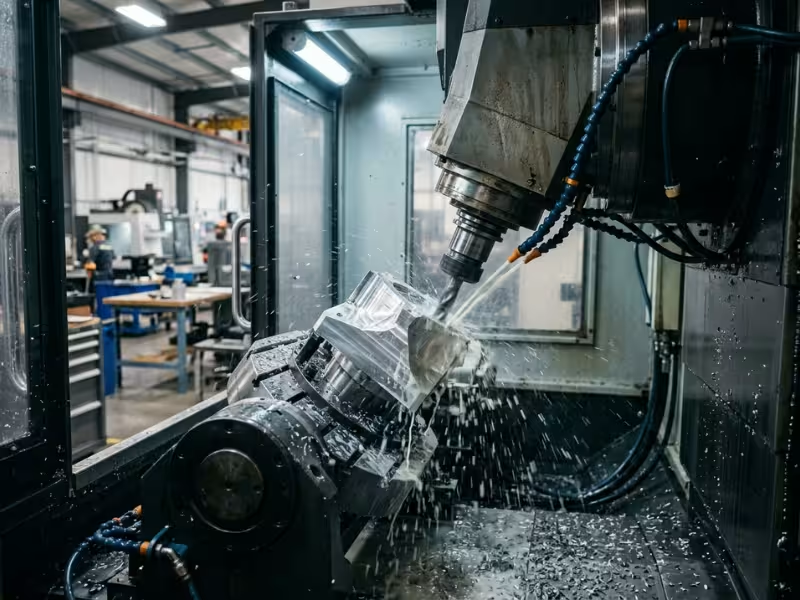
CNC machining works the other way. A cutting tool removes material from a solid block, guided by your program. That opens the door to almost any shape you can draw. Complex pockets, angled faces, tight bores, and features that change along the part all fall within reach.
CNC also holds tighter tolerances and cleaner surface finishes than extrusion can manage on critical faces. And when your design shifts, you just update the program. No die to scrap. No tooling to rebuild. That makes CNC a strong friend during prototypes and design changes.
The trade is just as clear. There is no die cost, but there is no volume discount either. CNC charges by time. Cycle time, setup, and fixturing drive the price, and that price barely moves whether you make ten parts or ten thousand.
The core tradeoff in one sentence
Read the comparison below before you go further. It frames the whole decision.
| Process | Best for | Main strength | Main limit |
|---|---|---|---|
| Extrusion | Constant profiles at high volume | Low per-part cost once the die runs | Locked to one cross-section |
| CNC machining | Complex shapes, tight specs, changing designs | Freedom and precision without tooling | Cost stays flat, never drops |
I have watched teams win by matching the process to the part instead of forcing the part onto a favorite method. When the shape stays the same and the numbers are big, extrusion earns its keep. When the shape gets clever or the tolerances get fussy, CNC pays for itself.
Here is the whole thing in one line: extrusion buys profile efficiency, and CNC buys geometric freedom.
The First Four Questions That Usually Decide the Process
Before you compare quotes or draw up dies, four simple questions do most of the heavy lifting. Answer them honestly, and the right process usually points itself out.
Does the part keep the same cross-section along its length?
Start here, because this one question rules out a whole path.
Picture cutting your part at any point along its length. Do you always see the same shape? If the cross-section stays constant, extrusion loves that part. A rail, a frame member, a heat sink profile, or a channel runs through a die beautifully.
Now look at the deal-breakers. Does the shape change as you move down the part? Do you need pockets carved into a face? Tapers that shrink one end? Undercuts that hook back on themselves? Wall sections that thicken and thin in different spots?
Any of those break the constant-profile rule. Extrusion cannot make them alone. That pushes you toward CNC, or toward a hybrid route where you extrude the blank and machine the tricky bits afterward.
So the first sort is clean. Same shape all the way through leans extrusion. Shape that shifts leans CNC or hybrid.
How many parts will you really buy per year?
Once you know the shape can survive the process, the next question is volume. Volume changes the math more than anything else.
Under 500 parts a year. A die rarely pays off here. You would carry the full tooling cost across too few units, and each part would swallow a big slice of it. CNC usually wins at this level.
500 to 5,000 parts a year. This is the gray zone. The answer swings on part complexity, alloy, and how much secondary machining the extrusion needs. Run the break-even numbers before you commit either way.
Over 5,000 parts a year. Now extrusion starts to shine. You spread the die cost across so many parts that it nearly disappears per unit. CNC keeps charging machine hours on every part, so high volume punishes CNC and rewards extrusion.
Be honest about the real yearly number, not the hopeful one. I have watched teams justify a die on a forecast that never arrived.
How tight are the critical tolerances and surface finish?
Not every dimension needs to be tight. Find the few that do, because they often decide the process on their own.
Extrusion holds decent tolerances, but they widen as the part gets longer. Metal moves, cools, and stretches through the press. A tolerance that looks fine on a short sample can drift across a long length.
CNC handles tight work far better. Mating faces, precise holes, bearing bores, and sealing surfaces all benefit from machining. When a feature has to line up perfectly with another part, CNC earns its cost.
Surface finish follows the same logic. Extrusion gives you a serviceable finish straight off the press, good enough for many uses. But smooth, controlled, spec-driven finishes on critical faces call for machining or a finishing step.
Here is my rule. If your tight tolerances live on a handful of features, extrude the profile and machine just those spots. If tight tolerances cover the whole part, CNC is probably your home.
How likely is the design to change?
The last question looks ahead. A die is a commitment. Once you cut it, changing the shape means cutting a new one or living with what you have.
If your design still shifts, hold off on tooling. Every revision after the die is made risks scrap, rework, or a full die rebuild.
CNC shrugs off changes. You update the program and run the next batch. That flexibility makes machining the smart pick during prototyping, early production, and any phase where engineering keeps tweaking things.
Extrusion rewards patience. Once the geometry is frozen and signed off, the die becomes a long-term asset that prints cheap parts for years.
Putting the four answers together
No single question decides everything. But read together, they narrow the field fast.
| Question | If the answer is this | Process usually favored |
|---|---|---|
| Same cross-section along the length? | Yes, constant profile | Extrusion |
| No — pockets, tapers, undercuts, changing walls | CNC or hybrid | |
| Parts per year? | Under 500 | CNC |
| 500–5,000 | Run break-even math | |
| Over 5,000 | Extrusion | |
| Critical tolerances and finish? | Tight on a few features only | Extrusion + secondary machining |
| Tight across the whole part | CNC | |
| Likely to change? | Design still shifting | CNC |
| Geometry frozen | Extrusion |
Work through all four before you ask for a single quote. They save you from expensive guesses down the line.
Geometry, Tolerance and Surface Finish — Where the Real Limit Shows Up
Both processes have a wall you eventually hit. Knowing where each one stops being smart saves you from paying for shapes the process cannot deliver well.
Where extrusion geometry stops being efficient
Extrusion only knows one trick, and it does it brilliantly: pushing a constant cross-section down the length of a part. Ask for anything that breaks that rule, and the process starts to strain.
Wall thickness sets the first hard limit. Push walls too thin, and the metal will not flow evenly through the die. You get uneven fill, warping, and dies that wear out fast.
Corners and internal voids test the process too. Sharp inside corners trap stress and slow the metal. Hollow profiles with internal webs need bridge or porthole dies, which cost more and complicate every step.
Then there is the feature problem. Holes, pockets, slots, and anything that interrupts the profile cannot come from the die. Those features arrive later through machining.
Where machining starts to get expensive
CNC can cut almost anything, but “can” and “should” are not the same.
Deep pockets top the list. The deeper you cut, the longer the tool reaches, and long tools bend. That forces slower feeds, more passes, and longer cycle times.
Thin walls fight you the same way. As the tool cuts, a thin wall flexes away from it. That flex causes chatter, poor finish, and parts that drift out of spec.
Machine choice matters too. A 3-axis machine handles flat faces and simple pockets cheaply. But once features wrap around multiple sides or sit at odd angles, you need 5-axis work. That machine costs more per hour and demands smarter programming.
When a few critical features justify secondary machining
This is where the two processes shake hands. You extrude the profile, then machine only the spots that truly need it. Done right, this gives you extrusion economics with CNC precision.
Some features almost always earn that second step:
- Tight holes. Bores that need real accuracy or a snug fit for pins, bolts, or bearings.
- Sealing faces. Surfaces that must seal against a gasket or O-ring.
- Datum surfaces. Reference faces that other parts measure from.
- Threaded features. Threads for fasteners or fittings.
The trick is restraint. Machine only the features that need it, and leave the rest as the press made them.
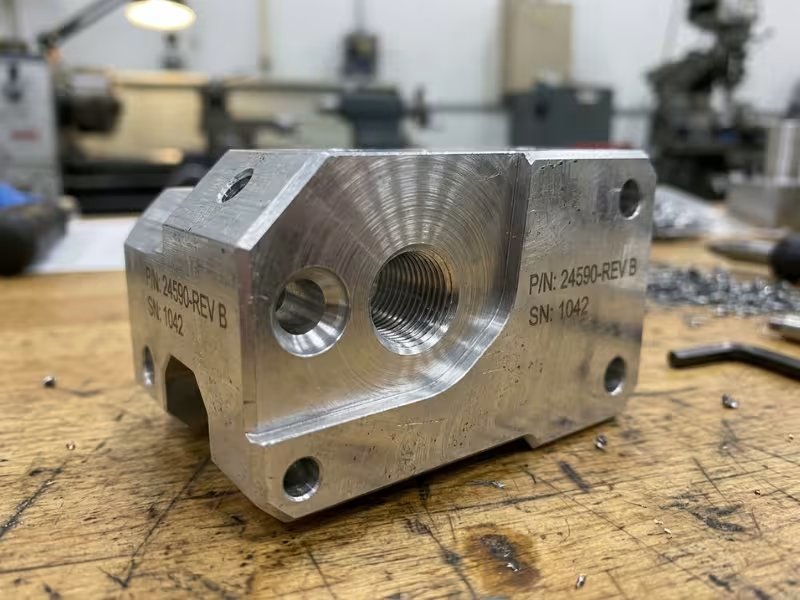
Matching features to the right process
Read the part feature by feature, not as one lump. A single part often spreads across all three columns below.
| Feature type | Extrusion | CNC machining | Hybrid |
|---|---|---|---|
| Constant profile / long runs | Excellent | Wasteful | Extrude the profile |
| Thin walls | Limited by minimum wall | Prone to chatter | Extrude, then trim carefully |
| Deep pockets | Not possible | Expensive | Machine after extrusion |
| Tight holes and bores | Not possible | Excellent | Extrude, then drill and ream |
| Sealing / datum faces | Rough finish only | Excellent | Machine only those faces |
| Threaded features | Not possible | Excellent | Cut threads after extrusion |
| Complex internal voids | Costly die work | Freeing but pricey | Case by case |
Use this to split your part into “let the die do it” and “let the cutter do it.” That habit alone prevents many expensive process mistakes.
Cost Breakdown — Where Extrusion Saves Money and Where CNC Does
Money is where most process debates get settled. But the cheaper quote is not always the cheaper part. You need to know what drives each cost and where the two paths cross.
Hard alloy extrusion cost drivers
Extrusion front-loads its cost. You pay big at the start, then cheap for the rest of the run.
Key drivers include:
- Die cost
- Billet price
- Press time
- Die trials
- Secondary machining
- Anodizing or other finishing
Simple solid profiles cost less. Hollow shapes with internal webs need more complex dies, and those cost more to cut and prove out.
CNC machining cost drivers
CNC spreads its cost across every part instead of loading it up front.
Key drivers include:
- Machine hourly rate
- Cycle time
- Programming
- Fixturing
- Tooling wear
- Inspection
The longer a part takes to cut, the more you pay. Deep pockets, thin walls, and tight features all stretch cycle time. Hard alloys also chew through cutters faster.
Break-even volume is the number that changes the answer
This is the heart of the decision. Extrusion carries a high fixed cost and a low per-part cost. CNC carries no die cost but a per-part cost that never really drops.
So there is a crossover point. Below it, CNC wins. Above it, extrusion wins.
Here is a simple example. Say your die costs $4,000. After the die, each extruded part costs $6 in material, press time, and finishing.
The same part on CNC costs $18 each. That $18 stays almost flat whether you make 10 parts or 10,000.
| Scenario | Extruded unit cost | Machined unit cost | Estimated crossover volume |
|---|---|---|---|
| Die cost | $4,000 (one-time) | $0 | |
| Per-part cost | $6 | $18 | |
| At 334 parts | $18 | $18 | ~334 parts |
| At 1,000 parts | $10 | $18 | Extrusion clearly wins |
| At 5,000 parts | $6.80 | $18 | Extrusion wins big |
Plug in your own numbers. The die cost and the per-part gap decide where your line sits.
What buyers often miss in quote comparisons
A quote rarely tells the whole story. The cheap number on the page can hide costs that land later.
Common misses include:
- Finishing
- Scrap and yield
- Secondary operations
- Tolerance-driven post-processing
Here is how the drivers stack up side by side:
| Cost driver | Extrusion impact | CNC impact | What the buyer should check |
|---|---|---|---|
| Tooling / die | High one-time die cost | No die cost | Die price and trial rounds |
| Material | Billet price, alloy-driven | Block or bar, more waste | Alloy grade and buy quantity |
| Run cost | Low per part at volume | Cycle time per part | Cost at your real volume |
| Setup / programming | Die trials up front | Programming and fixturing | One-time vs recurring split |
| Secondary ops | Often needed later | Usually built in | Is machining in the quote? |
| Finishing | Extra line item | Extra line item | What surface treatment is included |
| Scrap / yield | Rises with tight specs | Rises with hard alloys | Expected yield rate |
Compare true total cost per part, not the sticker price. Add every step, then run your break-even.
Lead Time, Tooling, and Design Change Risk
Cost gets the headlines, but timing quietly makes or breaks a project. The process you pick sets your clock the moment you say go, and it decides how much a late change hurts.
Why extrusion starts slower
Extrusion asks you to wait before you gain speed. The die comes first, and building it takes real time.
You start with die design. Then comes die fabrication. Then trial runs. Only after all that do you reach first article approval.
So extrusion’s timeline is slow up front, then fast for every part after that.
Why CNC starts faster
CNC skips the die entirely.
No die means no weeks of tooling. You go straight from a proven program to cutting metal. That head start makes CNC the natural pick for prototypes and urgent builds.
What drives your CNC timeline instead? Scheduling and setup. Getting machine time on a busy shop floor, then fixturing and dialing in the first part — that is where the days go.
What happens when engineering changes arrive late
This is where the two paths split hard.
A die is frozen steel. Change the geometry, and you either revise the die or cut a new one. That costs money and burns time.
CNC shrugs it off. You edit the program, run the next batch, and move on.
My advice stays simple. Freeze your geometry before you tool a die. If the design still moves, lean on CNC until it settles.
| Factor | Extrusion | CNC machining | Hybrid |
|---|---|---|---|
| Time to first part | Slow — die design, build, and trials come first | Fast — no die, straight to cutting | Medium — die up front, machining after |
| What drives the timeline | Die fabrication and trial runs | Scheduling and setup | Die build plus machining setup |
| Prototypes and urgent builds | Poor fit | Excellent fit | Rarely worth it |
| Cost of a late design change | High — die revision or rebuild | Low — edit the program | Medium — depends which feature changes |
| Scrap risk on late changes | High — old parts and die wasted | Low — little to throw away | Moderate — profile locked, features flexible |
| Best when design is | Frozen and signed off | Still shifting | Profile stable, details in flux |
Read this before you set your schedule. Extrusion rewards patience and a settled design. CNC rewards speed and forgives change.
Alloy and Temper Selection Can Eliminate One Option Early
Before you argue about geometry or cost, look at the metal itself. Sometimes the alloy and temper you need rule out a process on their own.
Not every alloy behaves well in both processes
Some alloys flow through a die like a dream. Others fight you.
The 6000 series leads the friendly camp. Alloys like 6061 and 6063 extrude easily, hold decent detail, and machine well too.
Step up to 7075 or 2024, and the story shifts. These high-strength alloys extrude slower, need more press force, and demand tighter control. They still machine well, but the extrusion route gets fussier and pricier.
Then come titanium and other hard alloys. These change the economics fast. They are tough on dies, tough on cutters, and slow to run either way.
Temper affects both machinability and final properties
Temper sets the alloy’s strength and hardness. It shapes how the metal cuts and how it performs in service.
In simple terms:
- T4 is softer and easier to form
- T5 is a practical balance for many extruded profiles
- T6 gives higher strength but makes machining harder
Sequence matters. Machine in a softer temper, then heat-treat, and the part can move. Machine after T6, and you fight a harder material.
Sometimes the material picks the process first
This point trips up many teams. If your alloy and process do not pair well, geometry comes second.
Confirm the alloy-process fit first. Then talk shape, tolerance, and volume.
| Alloy | Extrudability | Machinability | Typical note for buyers |
|---|---|---|---|
| 6063 | Excellent | Good | First choice for clean profiles |
| 6061 | Good | Very good | Great all-rounder for both routes |
| 7075 | Fair | Good | Strong, but extrusion runs slow and costs more |
| 2024 | Fair | Good | High strength, process-sensitive |
| Titanium | Poor | Poor | Costs jump fast — rethink the whole plan |
Match the metal to the process before anything else. Get this pairing right, and every later decision gets simpler.
The Hybrid Route Many Teams Miss
Most people treat this as a two-way fight: extrusion or CNC. But many of the smartest parts use both.
Extrude first, machine only what matters
The idea is simple. Let the die make the bulk of the part, then let the cutter finish the few features that need real accuracy.
You start with a near-net blank. The extrusion carries your profile down the full length, cheap and fast. Then you machine only the spots that demand it: tight holes, pockets, datum surfaces, and threads.
This saves you twice. You remove far less metal, so chip volume drops. And with less to cut, cycle time shrinks.
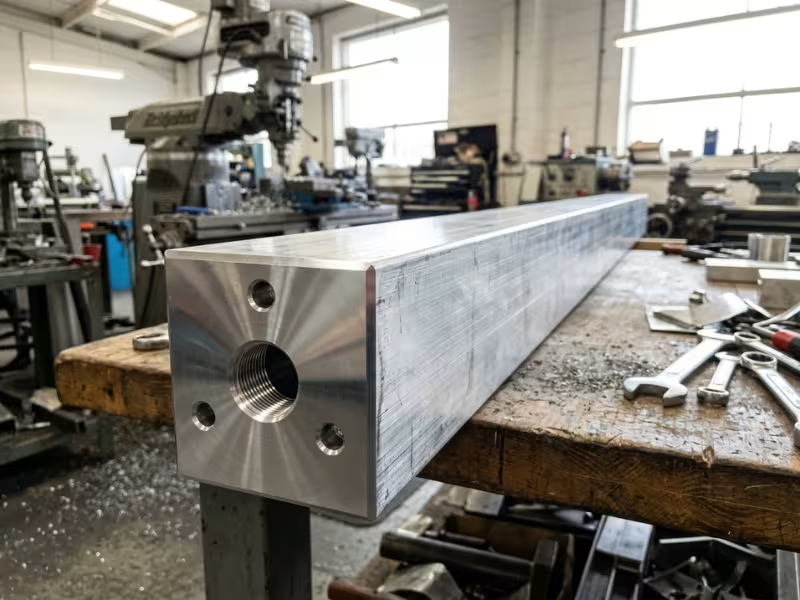
When hybrid works best
Some parts practically beg for this approach.
- Long parts with a repeated profile
- Critical features at the ends
- Structural profiles with local precision needs
In each case, the constant profile does the heavy lifting and machining handles the fussy bits.
When hybrid makes things worse
Hybrid is not a magic fix. Push it into the wrong job, and it can cost more than either process alone.
Low volume kills it. You still pay for the die up front. If you only need a small batch, that tooling cost never spreads far enough. In that case, straight CNC from solid stock usually makes more sense.
Loose extrusion tolerance causes fixture headaches. If the extruded blank varies too much, your machining fixtures cannot hold it the same way every time. Parts shift, critical features drift, and scrap climbs. When the blank is unstable, the machining step becomes harder than it should be.
An unstable design breaks the plan. Hybrid still needs a die. If your geometry keeps changing, that die becomes a liability, just like it does in a pure extrusion project. Freeze the profile first, then commit to the hybrid route.
Quick check: does hybrid fit your part?
Run your part against this before you commit.
| Part condition | Hybrid likely helps? | Why |
|---|---|---|
| Long part, repeated profile, few machined features | Yes | Die makes the body cheap, cutter finishes the details |
| Critical holes or faces at the ends only | Yes | Extrude the length, machine just the tips |
| Structural section with one tight mating area | Yes | Profile carries load, machining handles the fit |
| High annual volume | Yes | Die cost spreads thin, savings compound |
| Low annual volume | No | Die cost never pays off — go straight CNC |
| Loose or unstable extrusion tolerance | No | Fixtures cannot hold the blank, scrap rises |
| Design still changing | No | Die investment is too risky until geometry freezes |
The pattern is clear. Hybrid shines when you pair a stable profile with a few precise features and real volume.
A 10-Minute Decision Framework for Engineers and Buyers
You have seen all the pieces. Now put them to work. Grab your drawing, your annual volume number, and ten minutes.
Step 1–3: Volume, cross-section, critical features
Start with the three questions that filter fastest.
Step 1 — Count your real yearly volume. Under 500 parts leans CNC. Over 5,000 leans extrusion.
Step 2 — Check the cross-section. Same shape every time points to extrusion. Shape changes point to CNC or hybrid.
Step 3 — List the critical features. A few features on a mostly simple part points to hybrid. Tight tolerances all over the part point to CNC.
Step 4–5: Alloy, temper, and break-even math
Now confirm the material and the money.
Step 4 — Confirm the alloy and temper fit. Easy extruders like 6061 or 6063 keep both routes open. Harder alloys often tip the scale toward CNC.
Step 5 — Run the break-even math. Take the die cost, divide it by your volume, and add the per-part extrusion cost. Compare that total to the flat CNC price.
Step 6–7: Lead time reality and final process choice
The last two steps ground the choice in real-world timing.
Step 6 — Face the lead time reality. Urgent build? CNC usually wins. Frozen design and time to tool? Extrusion becomes safer.
Step 7 — Make the call. Read your seven answers together. If most point one way, trust them. When volume and cross-section favor extrusion but a few features need precision, choose hybrid.
Quick process selection worksheet
| Decision factor | Your part | Pushes toward extrusion / CNC / hybrid |
|---|---|---|
| Annual volume | _____ parts/year | Under 500 → CNC · Over 5,000 → Extrusion |
| Cross-section | Constant / changing | Constant → Extrusion · Changing → CNC or hybrid |
| Critical features | Few / spread everywhere | Few → Hybrid · Everywhere → CNC |
| Alloy fit | Easy / process-sensitive | 6061–6063 → Both open · 7075+ → CNC leans |
| Temper needs | T4 / T5 / T6 | T6 → Plan machining order |
| Break-even result | Extrusion or CNC cheaper | Cheaper number wins |
| Lead time and design | Urgent-changing / settled | Urgent → CNC · Settled → Extrusion |
Count the leans. Mostly extrusion means tool the die. Mostly CNC means machine it. A stable profile with a few precise features often means hybrid is your smartest bet.
Common Mistakes That Raise Cost Without Improving the Part
I have watched teams spend more and get less, all because of a few avoidable slips.
Choosing CNC for a constant-profile part because it feels simpler
CNC feels like the safe default. But if your part keeps the same cross-section down its length, machining it from solid burns money on every unit.
Opening a die before confirming the tolerance stack-up
A die is frozen steel. Cut it before you check how your tolerances stack across mating parts, and you risk a costly rebuild.
Over-specifying tolerances
Tight tolerances feel responsible. They are actually expensive. Every extra bit of precision adds machining time, inspection, and scrap risk.
Ignoring scrap and finishing in quote comparisons
The cheapest quote often hides the biggest bill.
| Hidden cost | What to check |
|---|---|
| Finishing | Is anodizing or coating included? |
| Secondary machining | Are holes, threads, and faces in the price? |
| Scrap and yield | What is the expected reject rate? |
Choosing alloy before checking process fit
Teams often pick an alloy for strength, then discover it fights the process. Confirm the alloy runs well in your chosen route before you lock it in.
Skip these five mistakes, and you spend money where it actually improves the part.
What to Send When You Ask for Quotes
Want a fast, accurate quote? Give your supplier everything up front.
Send these seven things:
- A drawing or 3D model
- Your expected annual volume
- Alloy and temper
- Critical tolerances
- Surface finish requirements
- Whether post-machining is allowed
- Your target lead time
Vague requests get vague prices. Clear requests get usable quotes.
FAQs
How do I know if my part can be extruded?
Slice your part anywhere along its length. If you always see the same shape, it can likely be extruded. A constant cross-section is the rule.
Which process is cheaper for 1,000 parts?
For a constant profile, extrusion usually wins at 1,000 parts. Spread the die cost across that volume, then compare it to the flat CNC price.
Can CNC machining match extrusion tolerances?
CNC does more than match them. On critical features, it usually beats them.
How long does it take to get an extrusion die made?
Plan for a few weeks, not a few days. The clock runs through die design, die fabrication, and trial runs.
Can I machine an extruded profile after it is produced?
Yes. In fact, that is often the smartest route. Extrude the profile, then machine only the features that need precision.
What alloys work well for both extrusion and CNC machining?
The 6000 series leads the pack.
| Alloy | Extrusion | CNC | Note |
|---|---|---|---|
| 6063 | Excellent | Good | First choice for clean profiles |
| 6061 | Good | Very good | Great all-rounder |
| 7075 | Fair | Good | Strong, but slow to extrude |
| Titanium | Poor | Poor | Costs jump fast |
The Bottom Line
Let’s bring it home.
A constant cross-section made in real volume? Extrude it. The die pays for itself, and your per-part cost keeps dropping.
Complex geometry, tight tolerances, or a design that still moves? Machine it. CNC gives you freedom and precision without locking you into tooling.
But do not treat hybrid as a backup plan. For many parts, it is the smartest choice, not the leftover one. Extrude the profile, machine only the features that need it, and you win on both cost and accuracy.
Here is the one move that saves you the most grief. Run your break-even math before you ask anyone for a quote. Take the die cost, divide it by your real yearly volume, add the per-part cost, and compare it to the flat CNC price.
Know your number first. Then request quotes. That order keeps you in control and stops expensive surprises before they start.