Estimating sheet metal prices is one of those skills that looks simple until it isn’t. Miss a line item, and you either lose the bid or ship every part at a loss. This guide walks through the cost elements, the math, and the common errors that quietly erode margin — using a single worked example to keep everything grounded.
What Goes Into a Sheet Metal Quote
Every quote draws from five cost buckets. The percentages shift with complexity and volume, but the structure stays the same.
|
Cost bucket |
What it covers |
Rough share of total |
|---|---|---|
|
Material |
Raw sheet, based on flat pattern area, thickness, and scrap |
20–40% |
|
Labor + Machine Time |
Cutting, bending, welding; burdened labor rate plus machine hour rate |
30–50% |
|
Tooling / Setup |
Programming, die work, first-article setup |
5–20% (high on short runs) |
|
Finishing |
Powder coat, anodize, plating; includes prep and masking |
10–25% |
|
Overhead + Profit |
Rent, utilities, admin, insurance, and your margin |
20–40% on top of direct cost |
The master formula:
Material + Labor + Machine + Tooling + Finishing + Overhead + Profit = Quote
Everything below either fills in one of those numbers or explains what makes it move.
Why Two Similar Parts Can Have Very Different Quotes
Before getting into the step-by-step calculation, it’s worth understanding what drives price differences. Two parts that look nearly identical on paper can come back with quotes that differ by 40% or more.
Material Choice and Thickness
The material choice is often the biggest single variable. Take one flat blank — roughly one square foot — and price it across three common materials:
|
Material |
Gauge / thickness |
Approx. price per lb |
Weight per sq ft |
Material cost |
|---|---|---|---|---|
|
Cold rolled steel |
16-ga (0.060″) |
$0.70–$1.00 |
~2.5 lb |
~$2.00 |
|
304 stainless |
14-ga (0.075″) |
$2.50–$3.50 |
~3.1 lb |
~$9.30 |
|
5052 aluminum |
0.063″ |
$2.80–$3.80 |
~0.9 lb |
~$3.00 |
Same footprint, very different costs. Stainless runs roughly five times the material cost of cold rolled steel on the same blank.
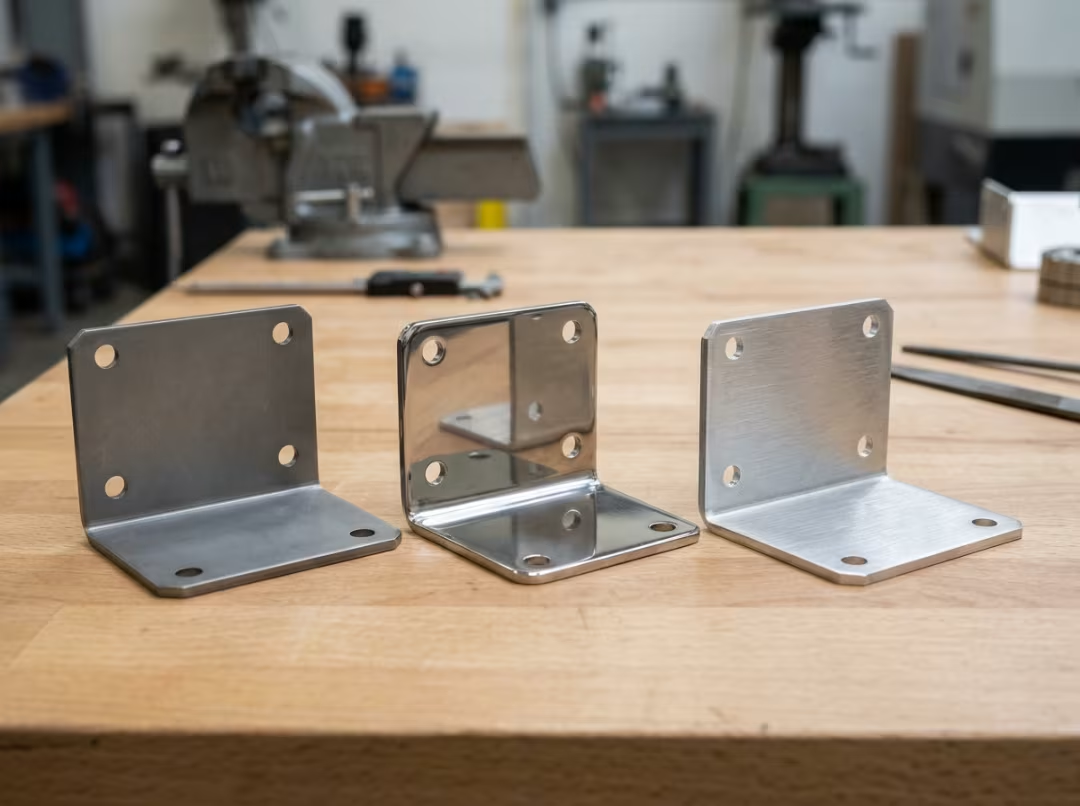
Thickness also carries a hidden second cost. Heavier gauge raises the bend tonnage required. Push past what a smaller press brake can handle and the job moves to a bigger machine with a higher hourly rate. So going thicker doesn’t just add weight — it can change which machine runs the part.
Production Volume
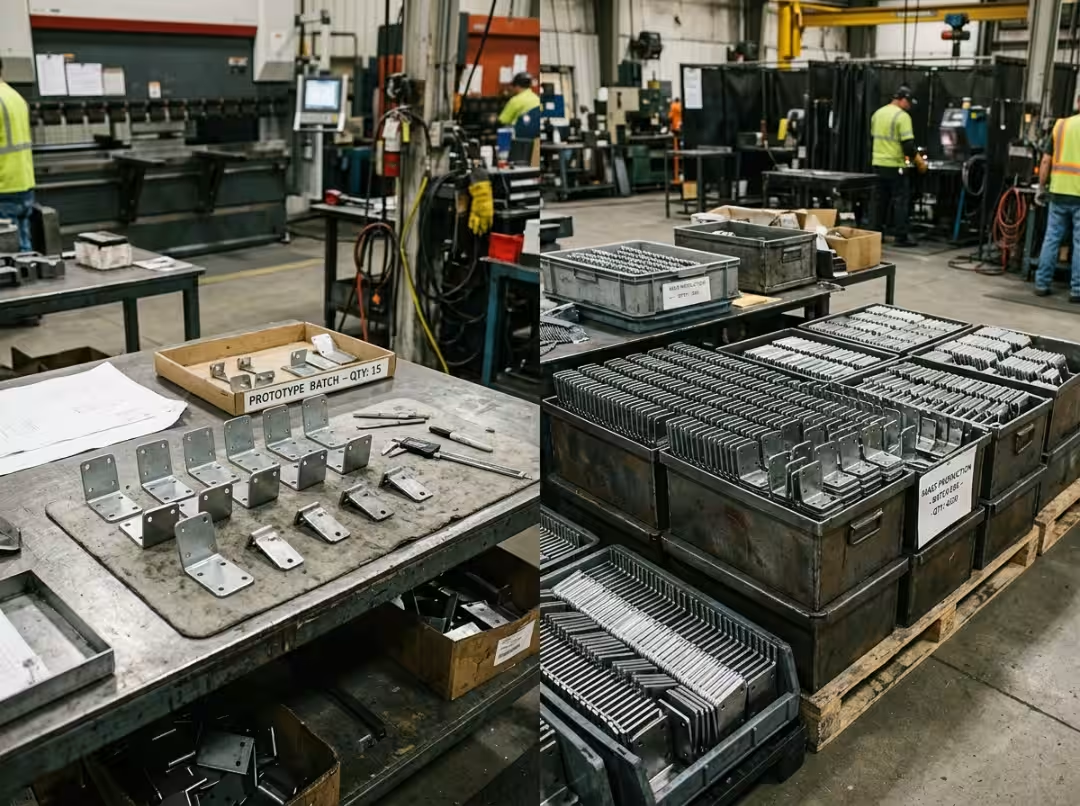
Setup and programming are fixed costs that spread across the run. A bracket requiring 30 minutes of programming at $75/hour costs $37.50 to set up, regardless of quantity:
|
Quantity |
Fixed cost per part |
Variable cost per part |
Total per part |
|---|---|---|---|
|
10 |
$3.75 |
$4.00 |
$7.75 |
|
500 |
$0.08 |
$4.00 |
$4.08 |
|
5,000 |
$0.01 |
$4.00 |
$4.01 |
The prototype run costs nearly double the production run. When a customer pushes back on a short-run quote, this is the conversation.
Part Complexity and Tolerances
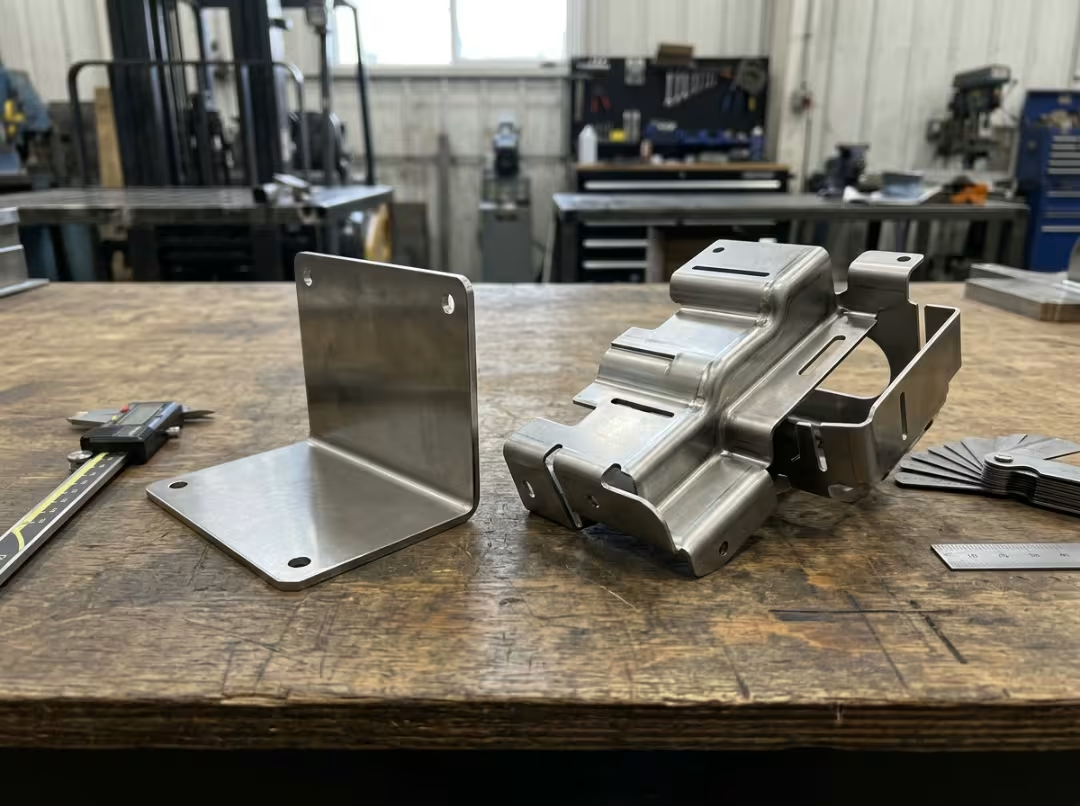
A two-bend part and a six-bend part with tight tolerances aren’t close to the same job. A standard ±0.015″ tolerance is straightforward. Tighten that to ±0.005″ and you’ve added inspection time, possibly a secondary machining step, and slower forming. Each extra bend also adds programming time and a handling step at the brake.
Hardware insertion — PEM nuts, standoffs — is a separate labor step that estimators routinely overlook. Eight inserts per part adds up quickly.
Finish Requirements
A basic powder coat is fast and forgiving. A clear anodize with masked threads and critical surfaces requires hand masking, careful racking, and a slower line to protect the finish. High-gloss and textured coatings add surface prep and more line time. The difference can push finishing cost several times higher than a plain coat.
How to Calculate a Sheet Metal Quote, Step by Step
The same bracket will serve as the working example throughout: an L-shaped bracket in 16-ga cold rolled steel (0.060″ thick), two 90° bends, four 0.25″ holes, powder coated black, quantity 250. One leg is 4″ tall, the other 6″ long, both 3″ wide.
Step 1 — Read the Drawing
Start by pulling the essentials: material type, thickness, finished dimensions, hole count, tolerances, finish, and quantity. Flag anything that triggers secondary operations — formed tabs, threaded inserts, tight callouts.
For this bracket: 16-ga CRS, 0.060″ thick, 4″ × 6″ × 3″, four holes, ±0.010″ tolerance, powder coat, no hardware. The tolerance is well within normal air-bend capability, so no secondary machining is needed.
Step 2 — Flat Pattern and Nesting
A bent part is longer than its finished legs combined, because metal stretches at the bend zone. The flat blank dimensions need to account for bend deduction.
For 16-ga steel with a standard air bend, a bend deduction of about 0.12″ per bend is realistic:
- Sum of legs: 4″ + 6″ = 10″
- Two bends: subtract 2 × 0.12″ = 0.24″
- Flat blank: 9.76″ × 3″
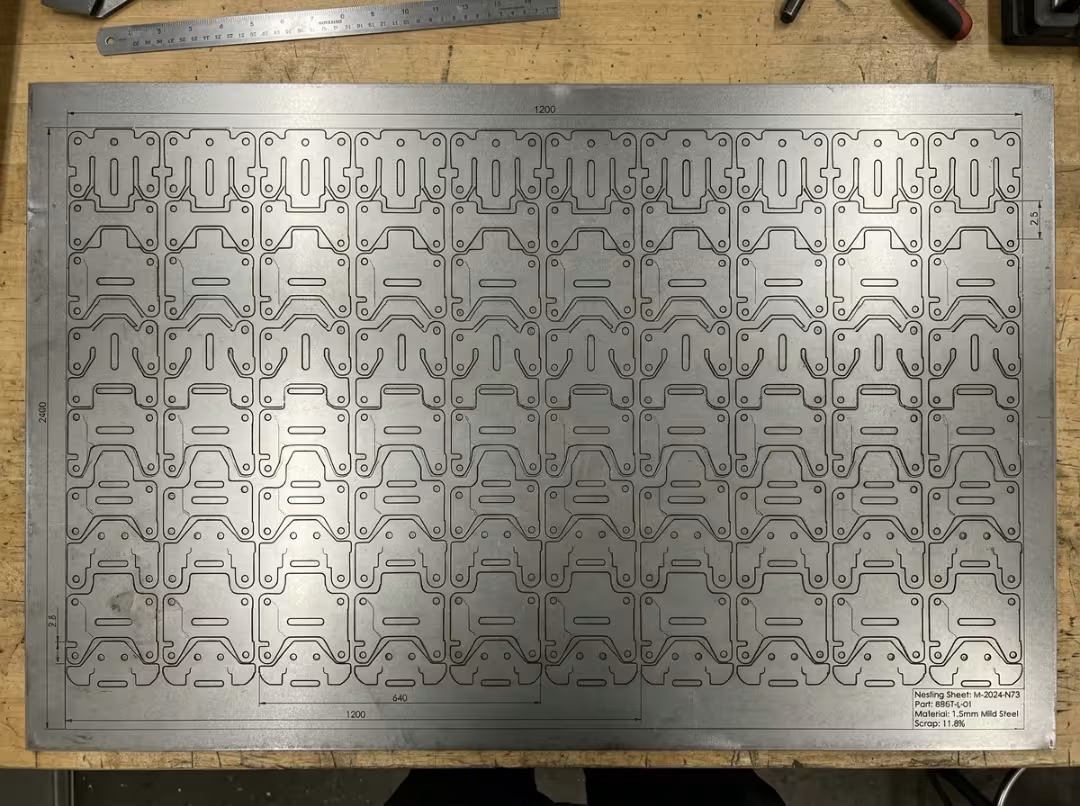
Now nest that blank on a 4′ × 8′ sheet (48″ × 96″). Allow 0.5″ between parts and a 0.5″ edge margin. Each part footprint with spacing runs about 10.26″ × 3.5″. A well-nested layout fits roughly 110 parts per sheet.
At 250 parts, you need 3 sheets (capacity for 330 parts), with the third sheet partially used. That leftover area factors into scrap.
Step 3 — Fabrication Time per Operation
Assign cycle times per operation for each laser cutting, bending, and deburring step:
- Laser cut: perimeter plus four holes on 16-ga steel — about 40 seconds
- Bend: two bends — roughly 25 seconds of forming
- Deburr: light hand deburr — about 30 seconds
Then add handling time: loading, unloading, repositioning between operations. It’s easy to shortchange this line. For this part, roughly 20 seconds per part is realistic — a detail that often gets overlooked in sheet metal forming and bending estimates.
Total touch time: about 1.9 minutes per part.
At a combined burdened labor and machine rate of $75/hour, that comes to $2.38 per part. On larger runs, operators pick up speed over time, but at 250 pieces the learning-curve effect is small enough to ignore.
Step 4 — Material Usage and Scrap
Net part weight:
- Flat area = 9.76″ × 3″ = 29.3 sq in
- Steel density = 0.283 lb/cu in
- Weight = 29.3 × 0.060 × 0.283 ≈ 0.50 lb per part
- At $0.85/lb: net material cost = $0.42 per part
But you don’t pay for the net part — you pay for the sheet. Three 4×8 sheets weigh about 234 lb, costing around $199. Divided across 250 parts, actual material cost is $0.80 per part — nearly double the net-weight figure. That difference is the skeleton, edge trim, and scrap you can’t avoid. Always quote off the sheet, not the part weight.
Step 5 — Finishing and Secondary Operations
Powder coat for this bracket — surface prep, racking, single matte coat — runs about $1.10 per part at this quantity. Deburring is already included in the labor line from Step 3. No hardware, no masking, so this step stays simple.
Step 6 — Sum, Apply Overhead, Add Profit
Programming and setup total 45 minutes at $75/hour = $56.25, spread across 250 parts = $0.23 per part.
|
Cost line |
Per part (qty 250) |
|---|---|
|
Material |
$0.80 |
|
Labor + Machine |
$2.38 |
|
Tooling / Setup |
$0.23 |
|
Finishing |
$1.10 |
|
Direct cost |
$4.51 |
|
Overhead (25%) |
$1.13 |
|
Cost before profit |
$5.64 |
|
Profit (20%) |
$1.13 |
|
Quoted price per part |
$6.77 |
At 250 pieces, the quote is roughly $6.77 per part, or $1,693 for the job.
Now run the same numbers at quantity 25. Material, labor, and finishing barely change. But the $56.25 of setup now spreads across only 25 parts — tooling jumps from $0.23 to $2.25 per part:
|
Cost line |
Per part (qty 25) |
|---|---|
|
Material |
$0.80 |
|
Labor + Machine |
$2.38 |
|
Tooling / Setup |
$2.25 |
|
Finishing |
$1.10 |
|
Direct cost |
$6.53 |
|
Overhead (25%) |
$1.63 |
|
Cost before profit |
$8.16 |
|
Profit (20%) |
$1.63 |
|
Quoted price per part |
$9.79 |
Same drawing, same material — but the small run costs 45% more per piece. Setup amortization is why volume conversations matter so much in this business.
The Errors That Quietly Erode Margin
Quoting off net part weight. If you base material cost on the finished part weight instead of what the sheet actually costs you, you’re missing the scrap entirely. In this example, that’s $0.42 versus $0.80 — nearly double. A sloppy nesting layout that drops utilization from 75% to 60% can add 10% or more to your material cost on a full run.
Gut-feel cycle times. Estimating from memory instead of tracking real production times leads to chronic under- or overcharging. In this example, assuming one minute of touch time instead of 1.9 minutes hides roughly $0.90 per part. Build standard times from actual runs and update them as your equipment changes.
Missing the invisible minutes. Handling, deburring, and inspection are easy to leave off a quote because they don’t happen at the main machine. But they showed up in the bracket example as about 50 seconds per part — close to $1.00. On tight-tolerance parts that need CMM or gauge inspection, add that time explicitly, or it disappears from your margin.
Ignoring tooling wear. Punches and dies dull with use. More burrs means slower forming, more downtime, and periodic maintenance. Adding even a few cents per part as a tooling allowance is far cheaper than absorbing the repair bill later.
Quick Shortcuts for Rough Estimates
When you need a ballpark number on the phone without running a full cost sheet:
Per-pound rule of thumb. For common steel parts with basic cutting and bending, a rough rate of $4 to $6 per pound covers material and simple fabrication. A half-pound bracket at $5/lb gives a $2.50 base — add overhead and profit from there. This works for straightforward steel parts. It breaks down fast for stainless, tight tolerances, or any significant finishing.
Nesting and quoting software. Tools like ProNest and NestingWorks calculate material utilization and cut times automatically, removing guesswork from the two biggest error sources. Most laser and punch machines also come with built-in quoting modules that pull cycle times directly from the program.
A reusable cost sheet. Build a spreadsheet with separate input fields for material, labor, machine, and finishing, plus formulas for overhead and profit. Change the quantity or material and the whole quote updates instantly. It’s the fastest way to answer “what if we go to 1,000 pieces?” without starting over.
Frequently Asked Questions
What’s a typical profit margin on a sheet metal job?
Most job shops target 15% to 35% on direct cost. High-volume, simple parts tend to run leaner because competition is tighter. Complex or low-volume work supports a higher margin.
What’s the difference between a budgetary estimate and a formal quote?
A budgetary estimate is a fast, rough number — useful before drawings are final. A formal quote is built from a complete cost sheet and is a price you’re prepared to hold. Never let a budgetary figure become a purchase order without re-running the numbers.
How does gauge affect the final price?
Heavier gauge means more material weight, so the material cost rises directly. It also increases bend tonnage requirements, which can shift the job to a larger press brake and slow down cycle time — so the cost impact is usually higher than the extra weight alone would suggest.
What costs do fabricators most often miss?
Handling time between operations, deburring, inspection on tight-tolerance parts, tooling wear, and the gap between net part weight and full sheet cost. Each one looks small in isolation. Together, they can add more than a dollar per part.
Conclusion
Sheet metal pricing is a process, not an instinct. Read the drawing, calculate the flat pattern, assign honest cycle times, count the real scrap, and build overhead and profit on top of a complete direct cost. Track your actual times and scrap rates so your standards reflect how your shop runs today, not how it ran two years ago. A price built on real data is one you can defend — and a customer who trusts your quotes tends to keep sending work.