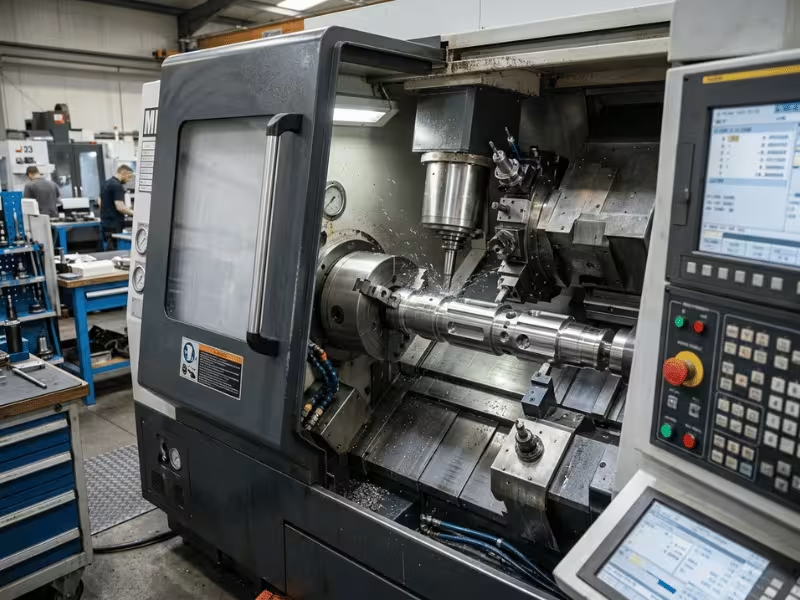
Some parts require you to fight on separate machines. You turn the shaft on a lathe, move it to a mill for the flats and cross holes, then chase tolerances that drift with every setup.
Each re-fixturing adds error. Each handoff adds wait time. And complex rotational parts suffer the most.
Mill-turn machining solves this. It combines turning and milling in one setup, so the part stays put while the machine does the rest.
I have quoted and run these jobs for years. I know when mill-turn earns its keep, and when it doesn’t.
This guide helps you decide if your parts belong on a mill-turn machine, or if a simpler setup still wins.
What Is Mill-Turn Machining?
Mill-turn machining runs turning and milling on one machine, in one setup. The workpiece spins for turning. Then powered tools spin to mill flats, cross holes, slots, and angled features. The part never leaves the machine.
It’s Not Just a Lathe With Live Tooling
Plenty of shops confuse the two, and that trips up quoting.
A lathe with live tooling can drill a few holes or cut a slot. Handy, but limited. A true mill-turn center brings a real milling spindle, a B-axis, and often a subspindle for back-side work. It handles complex geometry a live-tooling lathe simply can’t reach.
Why the Real Value Isn’t “More Features”
Here’s what I tell people who think mill-turn is about doing more on one machine.
The win isn’t extra capability. It’s fewer setups, shorter error chains, and fewer transfers between machines. Every time you re-fixture a part, you add error and lose time. Mill-turn cuts those handoffs down to one clamp.
That matters most on complex rotational parts, shafts, housings, fittings with features on several faces. Simple turned parts don’t need it. Match the process to the part, not the hype.
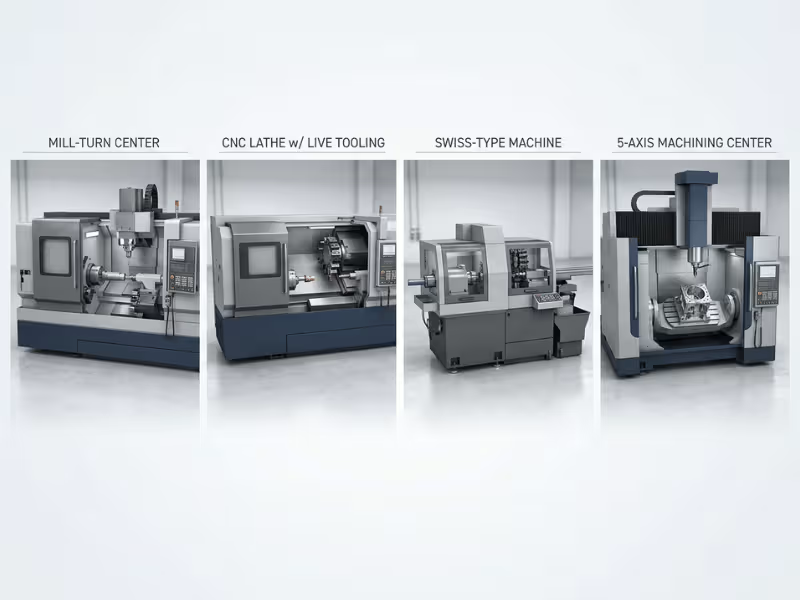
How Mill-Turn Differs From Other CNC Setups
Buyers often lump every multi-tasking machine into one bucket. That’s a costly mistake when you quote a job. Here’s how mill-turn stacks up against the setups people confuse it with.
|
Option |
Best for |
Main advantage |
Main limitation |
|---|---|---|---|
|
Mill-turn center |
Rotational parts with cross, angled, and back features |
One setup, short error chain |
Higher cost, complex programming |
|
Lathe with live tooling |
Turned parts needing a few holes or slots |
Cheaper, simple to run |
Limited milling and no true multi-axis |
|
Separate mill + lathe |
Shops with mixed, simpler work |
Lower entry cost, flexible |
More setups, tolerance stack-up |
|
Swiss machine |
Small, slender, high-volume parts |
Tight tolerances on tiny diameters |
Struggles with larger diameters |
|
5-axis machining center |
Prismatic block parts |
Great on solid, non-round shapes |
Weak on turned geometry |
Mill-Turn vs. Lathe With Live Tooling
Plenty of shops call a live-tooling lathe a mill-turn machine. It isn’t.
Live tooling drills a few holes or cuts a slot while the part sits in the chuck. Useful, but shallow. A true mill-turn center adds a real milling spindle, a B-axis, and often a subspindle for back-side work.
That means angled features, off-center pockets, and full back operations you can’t reach with basic live tooling. Quote the two as equals and you’ll promise tolerances you can’t hold.
Mill-Turn vs. Separate Milling and Turning Machines
Running a lathe and a mill as two stations feels flexible. On complex parts, it quietly drains time and accuracy.
Every transfer means a new clamp, a new reference, and fresh error. Those setups stack up, and so do the tolerances. You also carry more work-in-process, handle more, and use more floor space.
Mill-turn collapses that into one clamp. The part keeps its reference, so cross features line up and lead times drop. If your parts really only need one process, dedicated CNC turning or CNC milling may still be the smarter route.
Mill-Turn vs. Swiss and 5-Axis Machining
These serve different part shapes, so match the machine to the geometry.
When Mill-Turn Machining Makes Sense
Mill-turn shines on the right part and wastes money on the wrong one. So before you commit a job to it, run the part through a few honest questions.
A Quick Fit Check
Match your part to the table below before you quote or buy.
|
Situation |
Mill-turn fit |
|---|---|
|
Complex cylindrical parts with cross features |
Strong fit |
|
Parts needing front + back machining in one cycle |
Strong fit |
|
Low-to-medium volume with high complexity |
Strong fit |
|
Simple shafts with basic turning only |
Weak fit |
|
Small slender micro parts |
Consider Swiss instead |
|
Block-like parts from solid stock |
Consider 5-axis mill instead |
The pattern is clear. When a rotational part carries multi-face features, tight cross-face tolerances, or back-side work, mill-turn earns its cost fast. When the part is a plain shaft, a tiny slender pin, or a solid block, cheaper or better-suited machines win. Sort your parts this way and you’ll route each job to the machine that actually fits it.
How the Process Works in a Typical Job
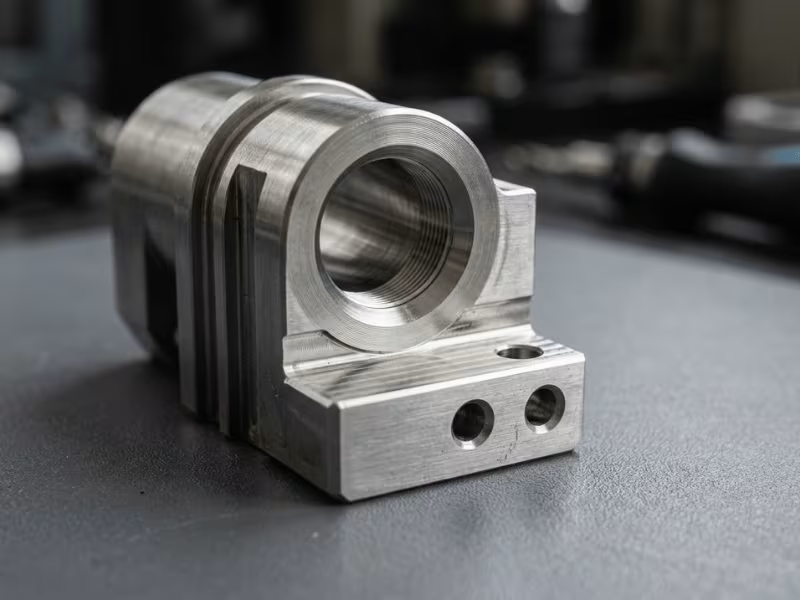
Let me walk you through a real part. Picture a hydraulic fitting: a round body with a threaded bore, cross holes, two wrench flats, and a finished back face.
The machine clamps the bar stock in the main spindle. It spins the part and turns the outer diameter, faces the end, and bores the center. All the round work happens first, in one grip.
Then the powered tools take over. The milling spindle drills the cross holes, cuts the flats, and machines any angled features. The part never moves. It keeps the same reference it had during turning, so those side features line up with the bore instead of drifting.
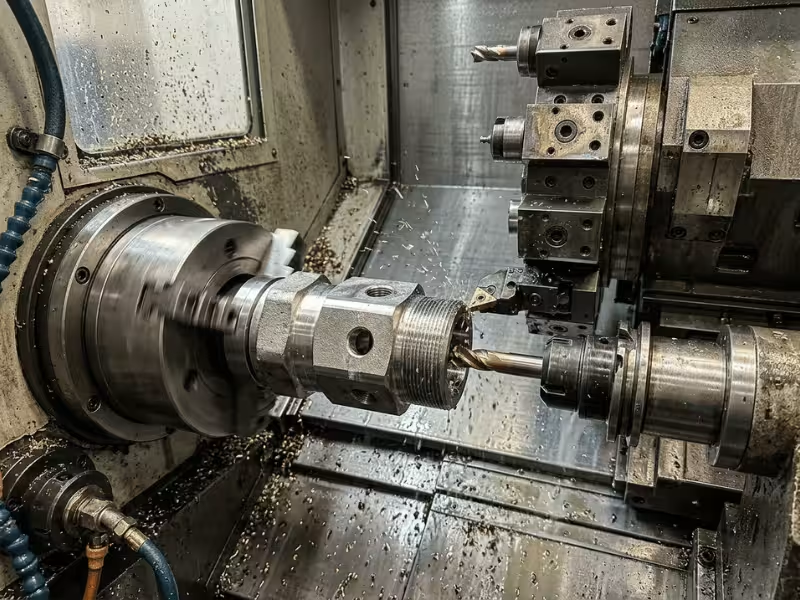
Next, the subspindle reaches in and grabs the finished end. It pulls the part off the main spindle in one smooth handoff. Now the back side faces the tools.
The machine finishes the back face, cuts a chamfer, and cleans up the second end. The part drops out complete.
One clamp did the front. One handoff did the back. No trip to another machine, no second setup sheet, no operator chasing tolerances across two stations.
That is why complex parts finish faster here. The time savings come from the setups you removed, not from cutting metal any quicker. And the accuracy holds because the part kept its reference the whole way through.
The Real Benefits — and Where They Actually Come From
Mill-turn gets sold on flash, but the real gains are quieter and more mechanical. Here’s where they actually come from.
Better accuracy through fewer setups
Mill-turn doesn’t make cuts more precise. It removes chances to lose precision.
Every time you re-clamp a part, you introduce drift. A slightly different reference, a hair of runout, a fresh alignment error. Those small shifts stack up across setups.
Keep the part in one grip and that error chain shrinks. Cross features line up with the bore because they were cut off the same reference. Fewer clamps, fewer drift points, tighter agreement between faces.
Shorter lead times on complex parts
The machine doesn’t cut metal faster. The whole job just moves faster.
On separate machines, a part waits in queue, gets turned, waits again, moves to the mill, waits some more. The cutting is a fraction of that timeline. The waiting eats the rest.
Lower handling and coordination cost
Two machines mean two schedules to coordinate. Someone has to move the part, track it, and slot it into the next station.
Every handoff is work-in-process sitting on a bench. Every transfer is a chance to lose a part, mix a batch, or stall on operator availability.
One machine finishing the part end to end kills most of that. Less shuffling between stations, fewer partial batches on the floor, and one operator owning the job instead of three coordinating around it.
Better fit for lights-out or unattended runs
This one comes with a condition. Mill-turn suits unattended work only when the part and the setup support it.
Pair a bar feeder with a subspindle and the machine can load stock, finish the front, transfer to the back, and eject a complete part, cycle after cycle, without hands on it. That’s real lights-out potential.
Match the part to the setup and mill-turn runs clean through a shift you’re not watching. Force it on the wrong job and unattended running becomes a gamble.
Where Mill-Turn Falls Short
Mill-turn earns a lot of praise, so let me balance the picture. On the wrong job, or in the wrong shop, it costs more than it returns.
Start with the price tag. A capable mill-turn center costs far more than a standalone lathe or mill. You pay for the subspindle, the B-axis, the milling spindle, and the tooling to feed them all. That upfront hit is real, and it scares off shops that never map it against actual part value.
But the machine price isn’t the trap most shops fall into. What they underestimate is programming maturity, tooling strategy, and operator readiness. Those three decide whether the machine ever pays back.
The tool is excellent. It just rewards shops that bring the skills, the tooling plan, and the right parts to it.
What Parts Are Best Suited to Mill-Turn
Before you quote a job, ask one question: does the part have a round core plus features on other faces? That combination is the signal.
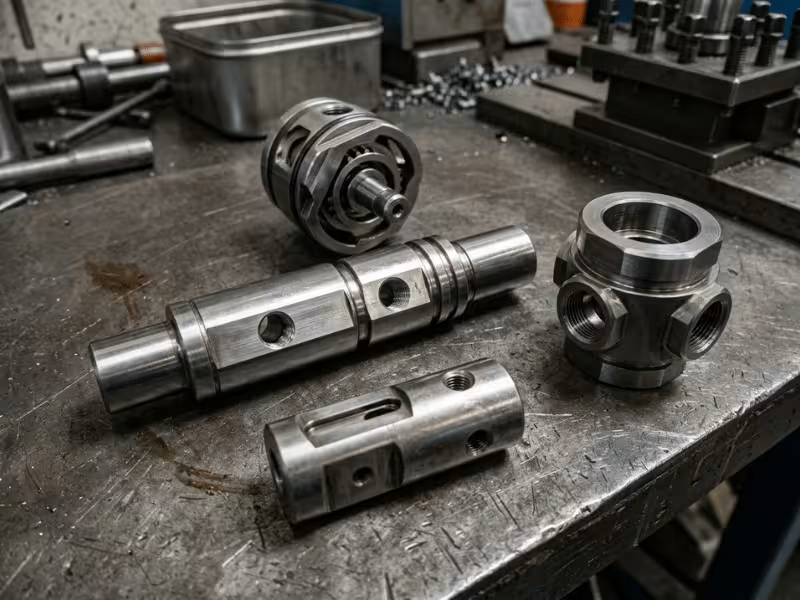
Mill-turn thrives on rotational base geometry, a shaft, hub, or cylinder, that also carries off-axis work. Cross holes, flats, angled bosses, eccentric pockets, and back-side features all point to a strong fit. The rounder and more complex the part, the more setups you save.
If the part is a plain shaft with only turned diameters, it doesn’t belong here. Save that for a standard lathe.
Here are the part types I route to mill-turn most often.
|
Part type |
Why mill-turn works well |
|---|---|
|
Shafts with milled flats and cross holes |
Turns the diameters, then mills the flats and holes off the same reference, so features stay aligned |
|
Housings with turned OD and off-center features |
Handles the round body and the eccentric pockets or bosses in one clamp |
|
Connectors and fittings |
Turns the bore and threads, then cuts wrench flats and cross ports without a second op |
|
Valve components |
Combines tight bore work with cross-drilling and seat features in a single cycle |
|
Medical and aerospace precision rotational parts |
Holds cross-face tolerances by keeping the part in one setup, exactly what these tolerances demand |
Notice the pattern. Every winner starts round and needs work on more than one face.
Match the geometry, not the industry, and you’ll route each part to the right machine.
How to Decide Whether Mill-Turn Is Worth It
The real question isn’t whether mill-turn is good. It’s whether your part’s complexity pays back the higher cost of programming and equipment. Run each job through five honest questions, and the answer usually sorts itself out.
Start with setups. Count how many times you clamp the part today across all machines. If a part touches three or four setups to finish, mill-turn starts looking cheap. Every setup you erase saves labor, time, and a chance to lose your reference.
Next, look at the features. Does the part need back-side work or angled cuts you can’t reach in one grip? Those jobs are exactly where a subspindle and B-axis pull their weight.
Then check your tolerances. When your tightest callouts tie features across faces, keeping the part in one clamp protects them. Scatter those tolerances across separate machines and you gamble on every re-fixture.
Now study your flow. If parts sit in queue, bounce between stations, or wait on a second operation, that idle time bloats your lead time far more than cutting ever does. Mill-turn collapses the wait, not just the machining.
Finally, weigh complexity against volume. A high-mix run of complex rotational parts justifies the programming hours. A handful of simple pieces won’t. The math turns on how often you reuse that hard-won setup.
Match your part to the table below.
|
Question |
If yes, mill-turn becomes more attractive |
|---|---|
|
How many setups does this part need right now? |
Three or more setups mean big savings from single-clamp completion |
|
Are there back-side operations or angled features? |
Subspindle and B-axis finish both ends in one cycle |
|
Do tight tolerances span multiple faces or references? |
One setup protects cross-face tolerances from re-fixture drift |
|
Is queue or wait time hurting lead time? |
Combining operations removes transfers and idle time between stations |
|
Does complexity plus annual volume justify the investment? |
Repeated complex runs spread programming and machine cost across more parts |
Read the pattern, not any single row. Answer “yes” to three or four of these and mill-turn likely recovers its cost fast. Answer “yes” to one at most, and a simpler setup still wins. Score your own parts this way before you spend a dollar.
Buying or Quoting Considerations
This section splits two ways. Buyers evaluating a machine and engineers sourcing parts need different questions, and both get shortchanged elsewhere.
If You Are Evaluating a Machine
Match the machine to your parts, not to the brochure.
If You Are Sourcing Mill-Turn Parts
Ask sharper questions than “can you make this?”
Which tolerances depend on single-setup control?</
A shop that knows this understands your part; one that shrugs will chase drift across re-fixtures.
Push on these four, and you’ll spot the shops that truly run mill-turn from the ones that just own the machine.
Best Practices for Better Mill-Turn Results
You picked the right machine for the part. Now here’s how to get the most out of it.
Get these five right, and the machine pays back every dollar you spent on it.
FAQ
The Bottom Line
Mill-turn belongs on complex rotational parts. If your part starts round and carries cross holes, flats, angled features, or back-side work, this is the machine for it.
So here’s the call. Complex rotational parts with off-axis features? Route them to mill-turn and let the single-setup advantage work for you. Plain turned shafts and simple pins? Leave them on a standard lathe, where they run faster and cheaper.
Match the part to the machine, and the choice makes itself. Which of your parts fits?